
Designing with HSS: How the ERW Manufacturing Process Works
Electric resistance welding (ERW) is the primary manufacturing process used to produce hollow structural sections (HSS) in North America. Each of the seven stages in an ERW tube mill, from coil entry through quality inspection, directly determines the dimensional accuracy, weld integrity, and mechanical properties of the finished section. Knowing what happens at each stage tells you exactly what you are specifying when you call out ASTM A500 on your construction documents.
Hollow structural sections are used as structural elements in buildings, bridges, and other structures across a broad range of sizes and wall thicknesses. They are produced in round, square, and rectangular profiles.
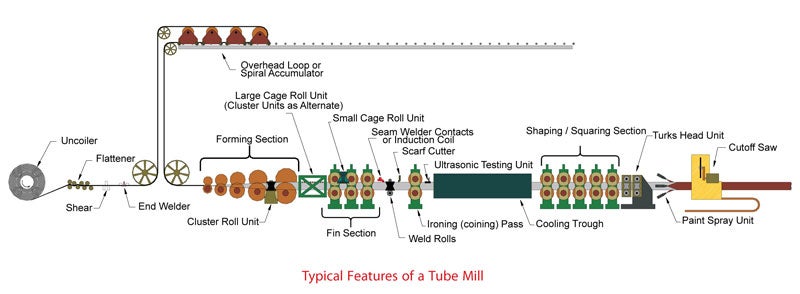
Stage 1: How Are Hot-Rolled Steel Coils Loaded and Prepared for the Tube Mill?
Every ERW tube mill begins with a hot-rolled steel coil: a continuous strip of flat steel produced at a steel mill and shipped in coil form to the tube mill. Coils typically come in standard widths. Coils will be cut, or slit, down to smaller widths that approximately match the perimeter of the HSS size that will be produced from that coil. The slitting process also prepares the edge of the coil for a successful electric resistance weld.
At the entry point, the coil is mounted on an uncoiler, which unrolls the strip and loads it into a machine that flattens the coil and preps it for butt-welding.
The leading end of the incoming strip must be joined to the tail end of the previous coil to maintain continuous production. Atlas Tube mills accomplish this with a welder and shear station that trims both strip ends square, then butt-welds them together. Strip preparation also includes a flattening or leveling station that removes the curvature (or “set”) the steel acquired from being coiled. Feeding crowned or wavy strip into forming rolls can affect the quality of the finished HSS, so a properly leveled entry strip is the first control point for finished tube tolerances.
Once the coil ends are attached, the coil is loaded into an accumulator. This machine holds several steel coils at one time and allows the downstream forming process to be continuous, while additional coils are butt-welded together.
Stage 2: How Does the Forming Process Shape Flat Strip into a Round Tube?
As the strip leaves the accumulator, it enters the forming section. The forming section is a progressive series of roll stands, each with a slightly different contour, that incrementally form the flat strip into a U-shaped profile. The continuous roll forming process includes a tooling sequence which typically includes breakdown rolls, fin passes, and side rolls.
Breakdown rolls make the initial bends to form the U-shape; fin passes and side rolls squeeze the strip edges toward one another to close the U-shape into a round shape and prepare the open seam for welding. The geometry of each roll pass is engineered so that no single pass introduces excessive strain at any one point. The result at the end of the forming section is a round tube with an open longitudinal seam, with the edges held close together and ready for the weld station.
Stage 3: How Does High-Frequency ERW Welding Join the Seam Without Filler Metal?
High-frequency electric resistance welding (HF-ERW) uses high-frequency electrical current and the natural resistance of steel to concentrate heat at the strip edges. As current flows along the converging edges of the strip toward the weld point, the electrical resistance of steel generates enough localized heat to bring the steel to a plasticized forging condition without the use of filler metal.
At that point, squeeze rolls (also called weld or pressure rolls) force the two heated edges together under controlled pressure. The plasticized metal at the interface of the strip edges is extruded through this pressure outward as flash, or “weld bead” on both the outside and inside surface. A properly controlled full thickness weld forms a continuous metallurgical bond through the seam with no filler metal added.
HF-ERW welding takes place continuously at mill line speed, and the heating-and-forging cycle occurs in a fraction of a second. Maintaining consistent power input, frequency, squeeze pressure, and line control is critical to producing uniform weld quality throughout the run.
External flash is removed immediately downstream of the weld station by a scarfing tool. Internal flash is typically left in place, as ASTM A500 tubing is commonly furnished without removal of inside flash. Atlas Tube can remove inside flash if a customer requires it, however.
Stage 4: How Are Sizing and Shaping Rolls Used to Achieve Final Dimensions?
The tube is still round when leaving the weld station, regardless of whether the finished product will be round, square, or rectangular. Sizing rolls bring the round tube to its final outside diameter for round HSS or reshape it into square and rectangular geometry.
For square and rectangular HSS, the round passes through a series of roll stands where the tube is progressively squeezed into a square or rectangular profile. Typical tooling is set up so that the outside corner radius for square and rectangular HSS is between 2 to 2.5 times the wall thickness. ASTM A500 has a maximum outside corner radius of 3 times the wall thickness.
Dimensional tolerances of the HSS are established and controlled at this stage. ASTM A500 lists the tolerances that must be met in the finished HSS. One of these tolerances is the maximum and minimum wall thickness of +/- 10%. AISC 360-22 Section B4.2 requires a 0.93 design thickness reduction factor for A500 HSS calculations to account for this tolerance. The properties listed in the AISC Manual already account for this design wall thickness, but it is important to make sure to account for this reduction when doing connection calculations. One easy way to do so is to design HSS connections in the Atlas Tube HSS Connections Hub™.
Stage 5: How Is HSS Straightened to Meet ASTM Tolerances?
After sizing, the tube passes through a straightening section. Turks head rolls, a set of four or more rolls arranged around the tube, apply controlled bending in multiple planes to remove camber, bow, and twist introduced by the forming and sizing process.
ASTM A500 specifies a straightness tolerance of 1/8 inch per every 5 feet of length (or the product of 1/8 inch times the total length in feet, divided by 5). For a 40-foot tube, that works out to a maximum permitted variation of 1 inch. Meeting that tolerance consistently requires that the Turks head rolls be properly set and that the incoming tube geometry from sizing is uniform.
Stage 6: How Is HSS Cut to Length at the Mill?
The continuous tube exiting the sizing and straightening section must be cut to discrete shipping lengths or to lengths specified by the customer. Mills use an automated cutoff system to make transverse cuts at the required mill length. Since the tube is moving continuously, the cutoff equipment travels with the tube during the cut, performing a flying cutoff. The cutting equipment produces a burr-free, square end.
Stage 7: What Inspection and Quality Control Steps Verify ERW HSS Before It Ships?
Structural certification does not occur only at the end of the mill; quality control is embedded throughout the process. Atlas Tube facilities employ several methods:
Destructive Testing: Periodic mechanical testing throughout the production run verifies yield strength, tensile strength, and elongation against specification minimums as well as weld integrity. Testing of a dog bone-shaped sample taken from the flat side of the finished HSS is performed in a Universal testing machine. This test verifies that the HSS meets the minimum specified yield and tensile strengths and the elongation.
Cone testing (expanding a sample over a mandrel) and flatness testing (pressing a sample flat with the weld at 0° and 90°) verify weld integrity. Reverse wedge testing is used for shaped sections too large for cone testing. The purpose of this destructive testing, which is required by the manufacturing specifications to be performed at a specified frequency, is to show that yielding or cracking occurs somewhere other than the weld.
Dimensional Checks: Wall thickness, outside dimensions, corner radii, twist, and straightness are measured against the permissible variations in ASTM A500 as applicable.
Mill Certification: Atlas Tube issues a Mill Test Report (MTR) for every bundle produced. Those reports include complete traceability back to the original coil, chemical analysis, tensile properties, and Charpy impact testing where applicable, backed by coil certificates from the raw-material supplier. The coil source and manufacturing process are also shown, along with recycled material content. This information can be useful when looking at sustainability or LEED related issues.
The cumulative effect of these controls (periodic destructive testing, dimensional verification, and full coil traceability) is what allows an engineer to call out an ASTM A500 designation on drawings and trust that the material delivered to the job site matches the specification.
Conclusion
The ERW tube mill is a tightly sequenced system where each stage — coil preparation, roll forming, HF-ERW welding, sizing, straightening, cut-to-length, and quality control — directly influences the dimensional accuracy, weld integrity, and mechanical properties of the finished HSS. When you specify ASTM A500 on your construction documents, you are specifying a set of process controls and minimum performance thresholds that apply to every tube on your project.
Atlas Tube is the only domestic producer offering the full range of Jumbo™ HSS sizes and maintains full material traceability from steelmaker to finished bundle, giving fabricators and project owners the documentation chain that demanding projects require.
For connection design resources, section properties, and column load tables for HSS, browse Atlas’ full suite of HSS comparison tools, typical details, and connection calculators or consult the STI Resource Library.
Brad Fletcher, Senior Structural Engineer at Atlas Tube, holds the S.E. license—structural engineering’s most advanced credential. With 30+ years of practice, he has served as an HSS industry liaison since 2011.